Automotive Die Castings
High pressure aluminium die cast parts for engine, powertrain, chassis and electric vehicle assemblies.
ExploreALUMINIUM HIGH PRESSURE DIE CASTING
Kılıçaslan works in aluminium high pressure die casting and die design. We do not just cast a part: we design its die, simulate the filling, machine it, measure it and hand it over ready to use.
WHY KILIÇASLAN
We design the die, we build it, and we cast the part on our own presses. Responsibility stays in one place: time to first article drops, and when something goes wrong there is no supplier in between.
END-TO-END PROCESS
The route followed from the moment your drawing reaches us until shipment. The output of each station is recorded as the input of the next, so when a deviation appears it is clear where it came from.
Part geometry, parting line and draft angles are reviewed for castability.
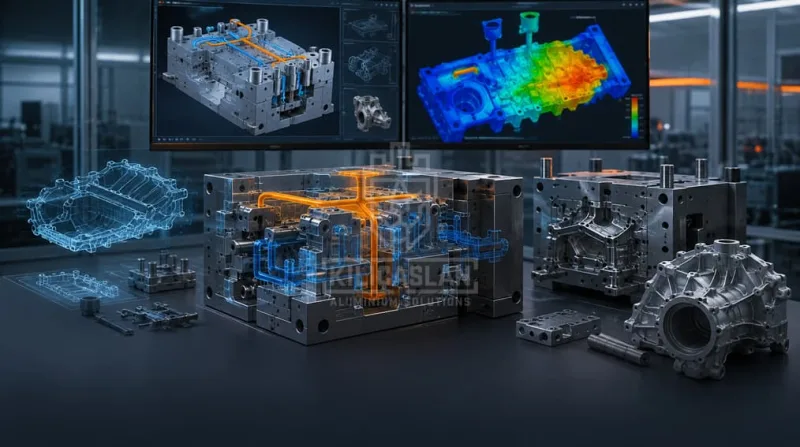
Runner and cooling design is verified by filling and solidification analysis before any steel is cut.
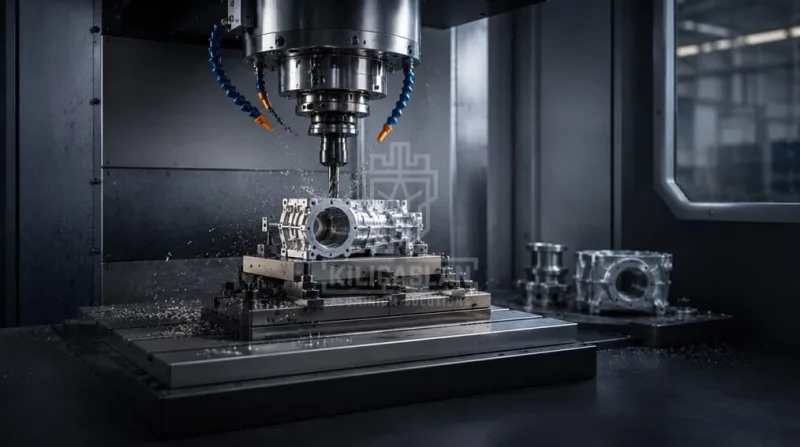
Die steel is machined, assembled and commissioned with a trial shot.
Series casting on a cold chamber press with process parameters under record.
Mating faces, holes and threads are machined on fixture.
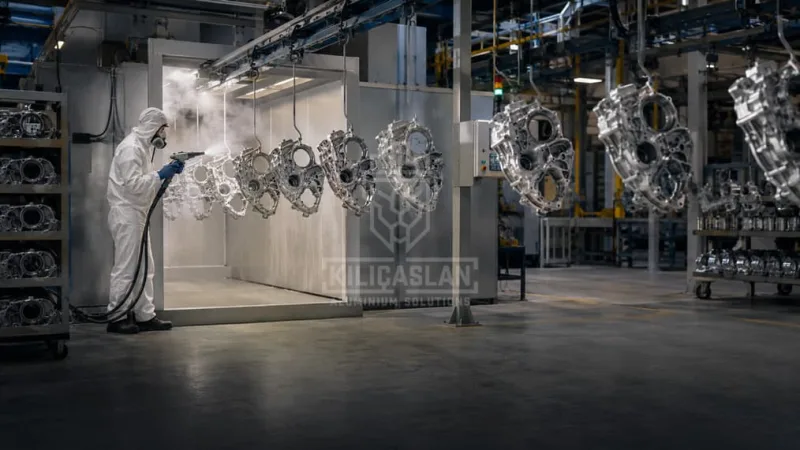
Deburring and blasting, then chromating, anodising or powder coating.
Packed and shipped after CMM measurement, leak testing and reporting.
Time from sample approval to series production depends on part geometry and die complexity; we settle it together during the feasibility review.
Discuss Your ProjectPRODUCT GROUPS
We produce aluminium die cast parts and tooling in six main groups. Each group brings its own tolerance, surface and testing expectations, and we set the process up accordingly.
High pressure aluminium die cast parts for engine, powertrain, chassis and electric vehicle assemblies.
ExploreAluminium die cast enclosure bodies for applications requiring sealing, EMC shielding and thermal management.
ExploreAluminium die cast luminaire bodies that carry heat away in LED lighting and withstand outdoor conditions.
ExploreDie cast bodies and mechanism parts where repeatability and surface quality lead in serial production.
ExploreDie cast bodies exposed to pressure and vibration, leak tested after machining.
ExploreIn house designed and manufactured die casting dies, gravity dies and inspection fixtures.
ExploreWe run the process without splitting it, from die design through assembly. That means one point of contact, one quality record and a shorter delivery chain.
Series production of thin walled, dimensionally stable parts on cold chamber presses.
ExploreRunner and cooling design verified by filling and solidification analysis before the first trial.
ExploreEvery step from die steel machining to trial casting is carried out in-house.
ExplorePost-casting machining, hole and thread operations, and surfaces requiring defined finish.
ExploreTrim die, automatic deburring and shot blasting to prepare surfaces before coating.
ExploreChromating, anodising and powder coating are run through an approved supplier network.
ExploreINDUSTRIES
We produce castings for industries ranging from automotive and lighting to home appliances and defence. Each one brings its own tolerance, testing and documentation expectations, and we set the process up accordingly.
PRODUCTION IN NUMBERS
The figures below are placeholders; replace them with your own data.
250–1650 t
Die casting machine clamping force range
120+
Dies in production
1800t/year
Annual casting capacity
0.05mm
Typical positional tolerance achieved
QUALITY APPROACH
Rather than sorting parts at the end, we aim to catch a deviation at the station where it appears.
Filling and solidification are simulated before any steel is cut, reducing porosity risk at the design stage.
Injection parameters are recorded, so when a deviation appears we can see which shot it began on.
CMM, spectrometer and leak test results are reported together with the part.
Casting batch, alloy analysis and measurement records can be traced back from the part.
Every finding from the field feeds into die and process revision.
Runners and aluminium scrap are recovered within our own cycle.
Short, practical articles on how design decisions shape the casting result.
FEASIBILITY REVIEW
Share your technical drawing or 3D model and we will come back on castability, die approach and estimated lead time.